


Xi'an Dongmeng Group Co., Ltd. is one of the most reliable manufacturers and suppliers of en 10305-1 e355 honed seamless steel tube in China, also supports customized service. With abundant experience, we warmly welcome you to wholesale cheap products in stock here and get free sample from our factory. For price consultation, contact us.
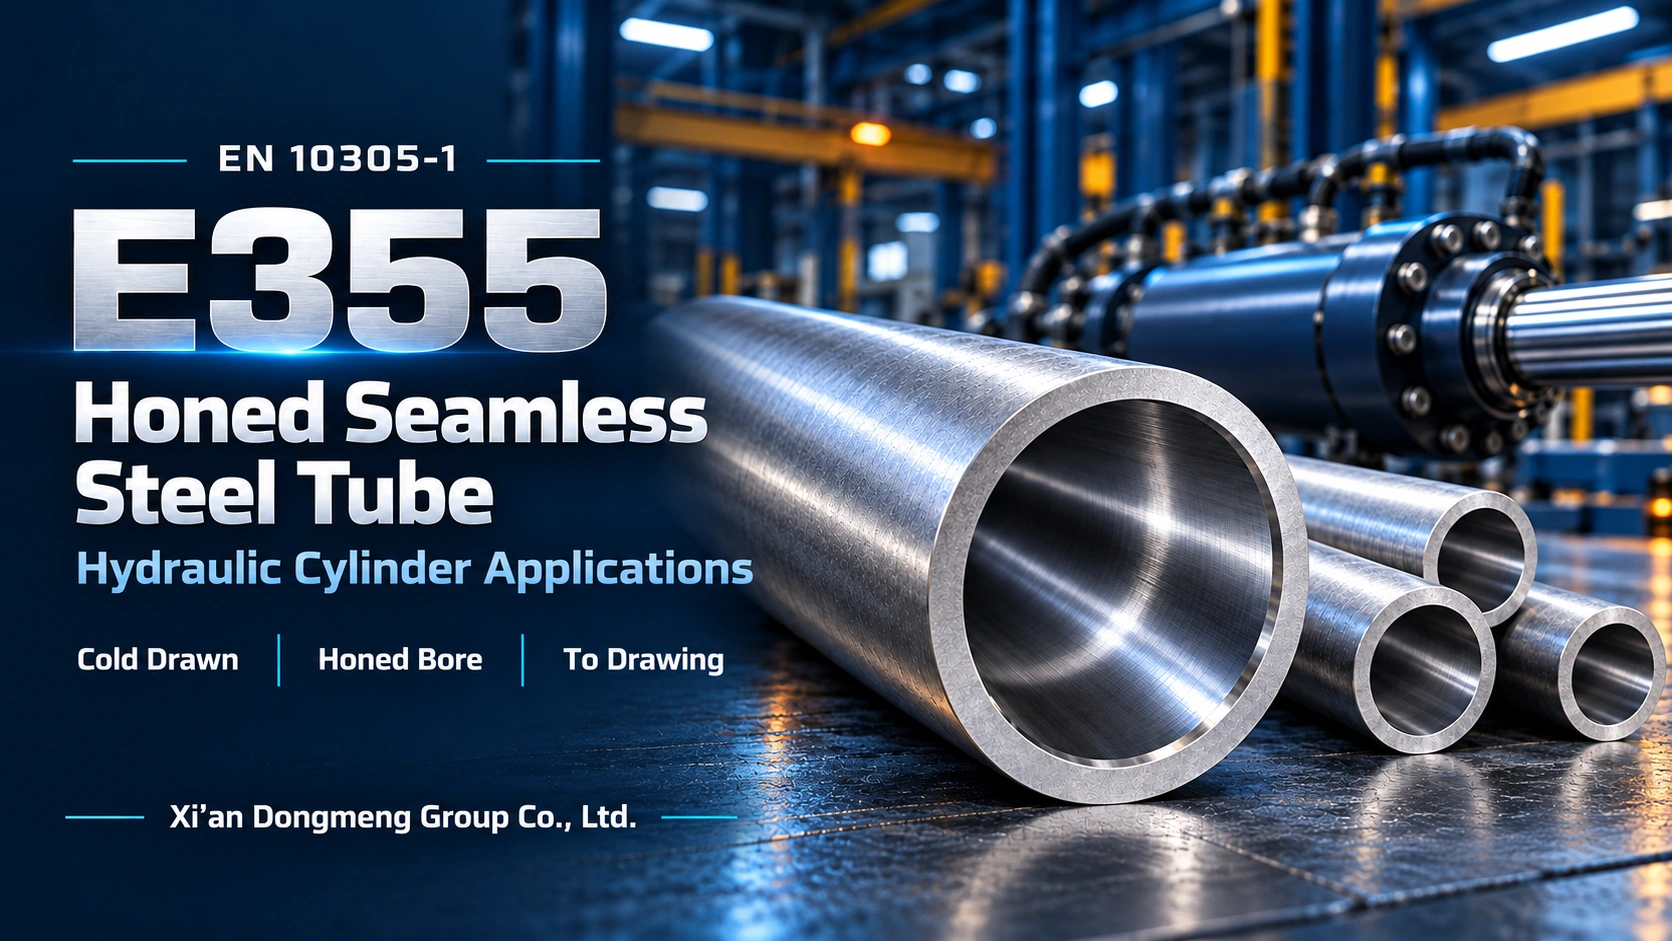
EN 10305-1 E355 Honed Seamless Steel Tube
Xi'an Dongmeng Group Co., Ltd. supplies E355 honed seamless steel tubes for hydraulic cylinder barrels, industrial actuators and precision mechanical components. Send your drawing for a quotation covering the required delivery condition, finished bore, outside diameter, length, end preparation and inspection documents.
E355, material number 1.0580, offers different strength and elongation requirements according to its delivery condition. Selecting the condition and finished-bore requirements together helps cylinder manufacturers purchase tubing that matches their fabrication and assembly process.
Why Specify E355 for Cylinder Barrels?
Higher specified strength than E235 in the same condition
E355 has higher listed tensile and yield strength requirements than E235 when compared in the corresponding delivery condition. This gives designers another material option when assessing barrel dimensions and loading requirements. Propriedades mecânicas (10305-1)
A finished bore matched to the component drawing
Purchasing a honed bore can reduce internal finishing work at the cylinder manufacturer when the supplied bore size, geometry and surface profile meet the assembly specification.
Clear acceptance requirements before production
Defining the finished ID, minimum remaining wall, surface texture and inspection scope allows buyers to compare quotations on the same technical basis.
Documentation aligned with incoming inspection
Agreeing on material certificates and finished-bore reports helps procurement and quality teams verify the supplied tubes against the purchase order.
E355+SR or E355+N?
The following selection guide uses the listed strength and elongation requirements to frame the decision.
| Condition | When to evaluate it | What to check |
|---|---|---|
| E355+SR | The design requires the higher listed yield strength of stress-relieved cold drawn tubing | Diameter-dependent yield requirement, fabrication sequence and final bore acceptance |
| E355+N | The design and fabrication requirements favour normalized material with higher specified elongation | Required strength, wall thickness, machining and welding procedure |
| Other conditions | The component drawing requires +C, +LC or +A | Condition-specific properties and subsequent processing |
Neither condition establishes a complete cylinder pressure rating. Confirm the choice against the component design and manufacturing process.
Need assistance with the condition? Send the existing drawing, material specification and intended fabrication steps with your inquiry.
Technical Specification
| Item | Specification |
|---|---|
| Product | E355 honed seamless steel tube |
| Technical delivery standard | EN 10305-1:2016 |
| Material number | 1.0580 |
| Tube form | Straight circular tube |
| Manufacturing route | Seamless, cold drawn |
| Delivery condition | Specified in the inquiry and purchase order |
| Internal finish | Honed; alternative finishing processes require agreement |
| Dimensions | OD × finished ID × length, or the dimension system on the drawing |
| Wall requirement | Nominal wall and minimum permitted wall after finishing |
| Bore tolerance | Drawing limits or an agreed ISO hole tolerance class |
| Geometry | Roundness, cylindricity and straightness where required |
| Surface texture | Ra and additional parameters required by the sealing system |
| Ends | Cut length, deburring, chamfers or machining as agreed |
| Documentation | EN 10204 inspection document and supplementary reports as ordered |
EN 10305-1 covers circular seamless cold drawn precision tubes with specified OD ≤380 mm. This is the standard's scope; available dimensions and processing feasibility are confirmed for each quotation.
Chemical Composition
The following base limits apply to cast analysis, expressed as mass percentages.
| C, max. | Si, max. | Mn, max. | P, max. | S, max. | Al total, min.* |
|---|---|---|---|---|---|
| 0.22% | 0.55% | 1.60% | 0.025% | 0.025% | 0.020% |
These E355 composition limits are also published in manufacturer technical data. Mannesmann
*The aluminium minimum has an exception where sufficient alternative nitrogen-binding elements are present. Relevant additions must be reported; when titanium is used, the standard requires verification that Al + Ti/2 ≥0.020%. hublebas.co.uk
Any additional chemistry requirements should be stated before material selection.
Mechanical Properties by Delivery Condition
Values below apply at room temperature. Strength values are in MPa; elongation is expressed as a percentage.
| Condition | Description | Tensile strength Rm | Yield strength ReH, min. | Elongation A, min. |
|---|---|---|---|---|
| +C | Cold drawn / hard | ≥640 | - | 4% |
| +LC | Cold drawn / soft | ≥580 | - | 7% |
| +SR | Cold drawn and stress relieved | ≥580 | 450* | 10% |
| +A | Soft annealed | ≥450 | - | 22% |
| +N | Normalized | 490–630 | 355** | 22% |
The condition-specific base values are confirmed by manufacturer data. Propriedades mecânicas (10305-1)
* E355+SR: For OD >160 mm, the specified minimum yield strength is 420 MPa.
** E355+N: When both OD ≤30 mm and wall thickness ≤3 mm, the minimum yield strength is 345 MPa.
"-" means the table does not give a separate fixed minimum yield value for that condition.
These dimensional exceptions follow EN 10305-1:2016 Table 4. Subsequent processing may change the mechanical properties.
Dimensions and Theoretical Weight
Specify the finished bore diameter, together with the outside diameter and minimum finished wall requirement.
For a circular tube:
Nominal wall = (OD − ID) ÷ 2
| Finished ID | Nominal OD | Calculated nominal wall | Theoretical mass |
|---|---|---|---|
| 40 mm | 50 mm | 5 mm | 5.55 kg/m |
| 80 mm | 100 mm | 10 mm | 22.20 kg/m |
| 100 mm | 120 mm | 10 mm | 27.13 kg/m |
| 140 mm | 170 mm | 15 mm | 57.34 kg/m |
| 160 mm | 190 mm | 15 mm | 64.74 kg/m |
| 200 mm | 230 mm | 15 mm | 79.53 kg/m |
| 250 mm | 290 mm | 20 mm | 133.17 kg/m |
These are calculated dimensional examples for inquiry preparation. Supply feasibility is confirmed in the quotation.
Mass calculation:
kg/m = π/4 × (OD² − ID²) × 0.00785
Diameters are in millimetres; assumed steel density is 7,850 kg/m³. Actual mass varies with dimensions and tolerances.
For design purposes, account for diameter tolerances, eccentricity, honing allowance and local machining when establishing the minimum remaining wall.
Finished Bore Tolerances
The following ISO hole tolerance examples show the relationship between nominal bore diameter and permissible size deviation.
| Nominal bore diameter | H7 | H8 | H9 |
|---|---|---|---|
| >30 to 50 mm | 0 / +0.025 mm | 0 / +0.039 mm | 0 / +0.062 mm |
| >50 to 80 mm | 0 / +0.030 mm | 0 / +0.046 mm | 0 / +0.074 mm |
| >80 to 120 mm | 0 / +0.035 mm | 0 / +0.054 mm | 0 / +0.087 mm |
| >120 to 180 mm | 0 / +0.040 mm | 0 / +0.063 mm | 0 / +0.100 mm |
| >180 to 250 mm | 0 / +0.046 mm | 0 / +0.072 mm | 0 / +0.115 mm |
| >250 to 315 mm | 0 / +0.052 mm | 0 / +0.081 mm | 0 / +0.130 mm |
For example, a 100 mm H8 bore has size limits of 100.000–100.054 mm. The tolerance widths follow ISO 286-2. ISO 286-2:2010
Choose the tolerance required by the piston and seal design. Manufacturing feasibility is reviewed against the bore diameter, tube length, wall and geometry requirements.
Surface Texture for Seal Performance
Specify the surface profile required by the selected seals, including:
Ra and Rz limits.
Material ratio Rmr where required.
Measurement settings, direction and locations.
Acceptance criteria for scratches, burrs and machining marks.
Seal manufacturers assess mating surfaces using more than Ra alone. Surface profile and material ratio can affect suitability even where roughness readings appear similar.
Honing, SRB and Subsequent Fabrication
Honing uses abrasive tools to remove material and finish the bore through rotational and reciprocating motion.
Skiving and roller burnishing-SRB uses cutting followed by roller burnishing. The process and resulting surface texture differ from abrasive honing. Sunnen – Sunnen Products Company
Identify the accepted finishing process in the order. Where a drawing specifies honing, review any proposed alternative against the required geometry and seal surface profile.
For welded or extensively machined barrels, discuss the fabrication sequence and the stage at which final bore acceptance will take place. Welding requirements should be assessed using the material composition, delivery condition, joint design and approved welding procedure.
Inspection and Documentation
Agree on the material and finished-tube inspection package before production.
| Record | What it should establish |
|---|---|
| Material inspection document | Grade, condition, material identification and agreed material test results |
| Dimensional report | OD, finished ID, length and wall requirements |
| Bore geometry report | Specified roundness, cylindricity or straightness checks |
| Surface texture report | Measured parameters and measurement settings |
| NDT report, when ordered | Method, coverage, acceptance level and results |
| Identification and packing records | Connection between supplied tubes, packing units and inspection documents |
Specify EN 10204 Type 3.1 when required. Also identify the finished-bore reports needed for incoming acceptance. EN 10204 document types are used together with the applicable product specification. en
For EN 10305-1 orders, longitudinal-imperfection NDT and leak-tightness verification can be specified under Options 12 and 13 respectively. Confirm the required method and acceptance criteria in the order. hublebas.co.uk
Third-party witnessing or additional inspection can be discussed before order placement.
Applications
| Buyer application | Main purchasing considerations |
|---|---|
| Construction machinery cylinders | Material condition, minimum finished wall and fatigue design |
| Agricultural equipment cylinders | Bore finish, seal compatibility and corrosion protection |
| Forklift and handling equipment | Bore dimensions, straightness and end machining |
| Industrial presses and actuators | Loading requirements, geometry and inspection scope |
| Cylinder repair and replacement | Original drawing, mating dimensions and material specification |
The allowable working pressure depends on the complete cylinder design, including temperature, cyclic loading, ports, joints and end connections.
Supply Support and Export Packing
Submit drawings for review of cut lengths, bore finishing, end preparation and inspection requirements. Processing scope and availability are confirmed in the quotation.
For repeat orders, provide the approved drawing revision and acceptance specification so that material, processing and documentation requirements remain consistent.
Agree on the protection and packing needed for transport and storage:
Temporary corrosion protection compatible with the subsequent process.
Bore and end protection.
Supports and separators to reduce handling damage.
Suitable bundles, crates or other agreed packing.
Identification linked to the order and material records.
Specify any cleaning, oil restrictions or destination packing requirements before shipment.
Frequently Asked Questions
1. Which condition should I choose: E355+SR or E355+N?
Compare the required strength, elongation and fabrication sequence. +SR has higher listed yield requirements; +N has higher specified elongation. Send the drawing if the condition is not yet defined.
2. How does E355 differ from E235?
E355 has higher listed strength requirements in corresponding delivery conditions. Their chemistry and elongation requirements also differ. Select the grade against the component design rather than substituting it solely by name.
3. Can EN 10305-1 and EN 10305-4 be used interchangeably?
They have different requirements. Part 4 covers seamless cold drawn tubes for hydraulic and pneumatic power systems and specifies normalized delivery. For E355, its base sulfur maximum is 0.015%, compared with 0.025% in Part 1. Confirm the required standard explicitly. hublebas.co.uk
4. Can I specify an H8 or H9 finished bore?
Include the required class or numerical bore limits in the drawing. The quotation should confirm feasibility for the selected bore diameter, length, wall and geometry requirements.
5. Can SRB replace a honed finish?
Review the proposed process against the component specification and seal requirements. Honing and SRB produce different surface textures; accept an alternative only after the relevant technical requirements have been checked.
6. Can E355 tubes be welded?
Assess welding using the actual composition, delivery condition, wall and joint requirements. The fabrication procedure should address any changes that could affect the required final properties or bore geometry.
7. What documents should I request?
Identify the EN 10204 document type, material traceability requirements and finished-bore reports. Request dimensional, surface texture and additional test records according to your incoming inspection plan.
8. Is ultrasonic testing included automatically?
State the NDT method, coverage and acceptance level in the inquiry. The inspection package should establish the tests required for the order rather than assume every tube receives the same testing.
9. What are the MOQ, price and lead time?
Commercial terms are confirmed for the required condition, dimensions, processing scope, inspection and quantity. Include trial-order and repeat-order requirements so that the quotation can address both.
10. What information is needed for an accurate quotation?
Send the condition, OD, finished ID and tolerance, length, quantity and destination. Attach the drawing and identify minimum wall, surface, end machining, inspection and packing requirements.
Request Your E355 Honed Tube Quote
Send your specification to Dongmeng Group for quotation and technical review.
| RFQ item | Information to provide |
|---|---|
| Material | E355 and required delivery condition |
| Dimensions | OD, finished ID, length and tolerances |
| Finished wall | Minimum requirement after processing |
| Bore finish | Accepted process and surface requirements |
| Processing | Cutting, chamfers, ends or machining |
| Quantity | Pieces, total length or weight |
| Inspection | Document type, reports and additional tests |
| Delivery | Destination, packing and required date |
Example inquiry
EN 10305-1 E355+SR honed seamless tube, OD 120 mm × finished ID 100 mm H8 × length 2,000 mm, quantity 50 pieces. Please quote against the attached drawing, including its surface texture, minimum wall, end preparation, EN 10204 Type 3.1 documentation and packing requirements.
Request an E355 Tube Quote
If some parameters are undecided, send the current drawing and identify the items requiring review.
Office Information
Xi'an Dongmeng Group Co., Ltd.
Phone: +86 15769214734
Email: office@dongmjd.com
WhatsApp: +86 15769214734
Office Address: Room 4107, Runfeng Building, Sanqiao New Street, Weiyang District, Xi'an, Shaanxi, China.
Contact information follows the published company contact page.
Hot Tags: E355 honed tube, EN 10305-1 E355 honed seamless steel tube, E355 hydraulic cylinder tube, E355+SR honed tube, E355+N seamless tube, 1.0580 precision steel tube, E355 cold drawn seamless tube, honed cylinder barrel tube, H8 honed tube, H9 cylinder tube, E355 honed tube supplier, custom honed steel tube, ASTM A519 Hydraulic Cylinder Tube, ASTM A519 4140 Honed Seamless Steel Tube For Hydraulic Cylinder, EN 10305 1 E355 Honed Seamless Steel Tube, ASTM A519 1045 Honed Seamless Steel Tube For Hydraulic Cylinder, EN 10305 1 C45E Honed Seamless Steel Tube, EN 10305 1 C35E Honed Seamless Steel Tube


