

Xi'an Dongmeng Group Co., Ltd. is one of the most reliable manufacturers and suppliers of astm a335 p92 pipe in China, also supports customized service. With abundant experience, we warmly welcome you to wholesale cheap products in stock here and get free sample from our factory. For price consultation, contact us.
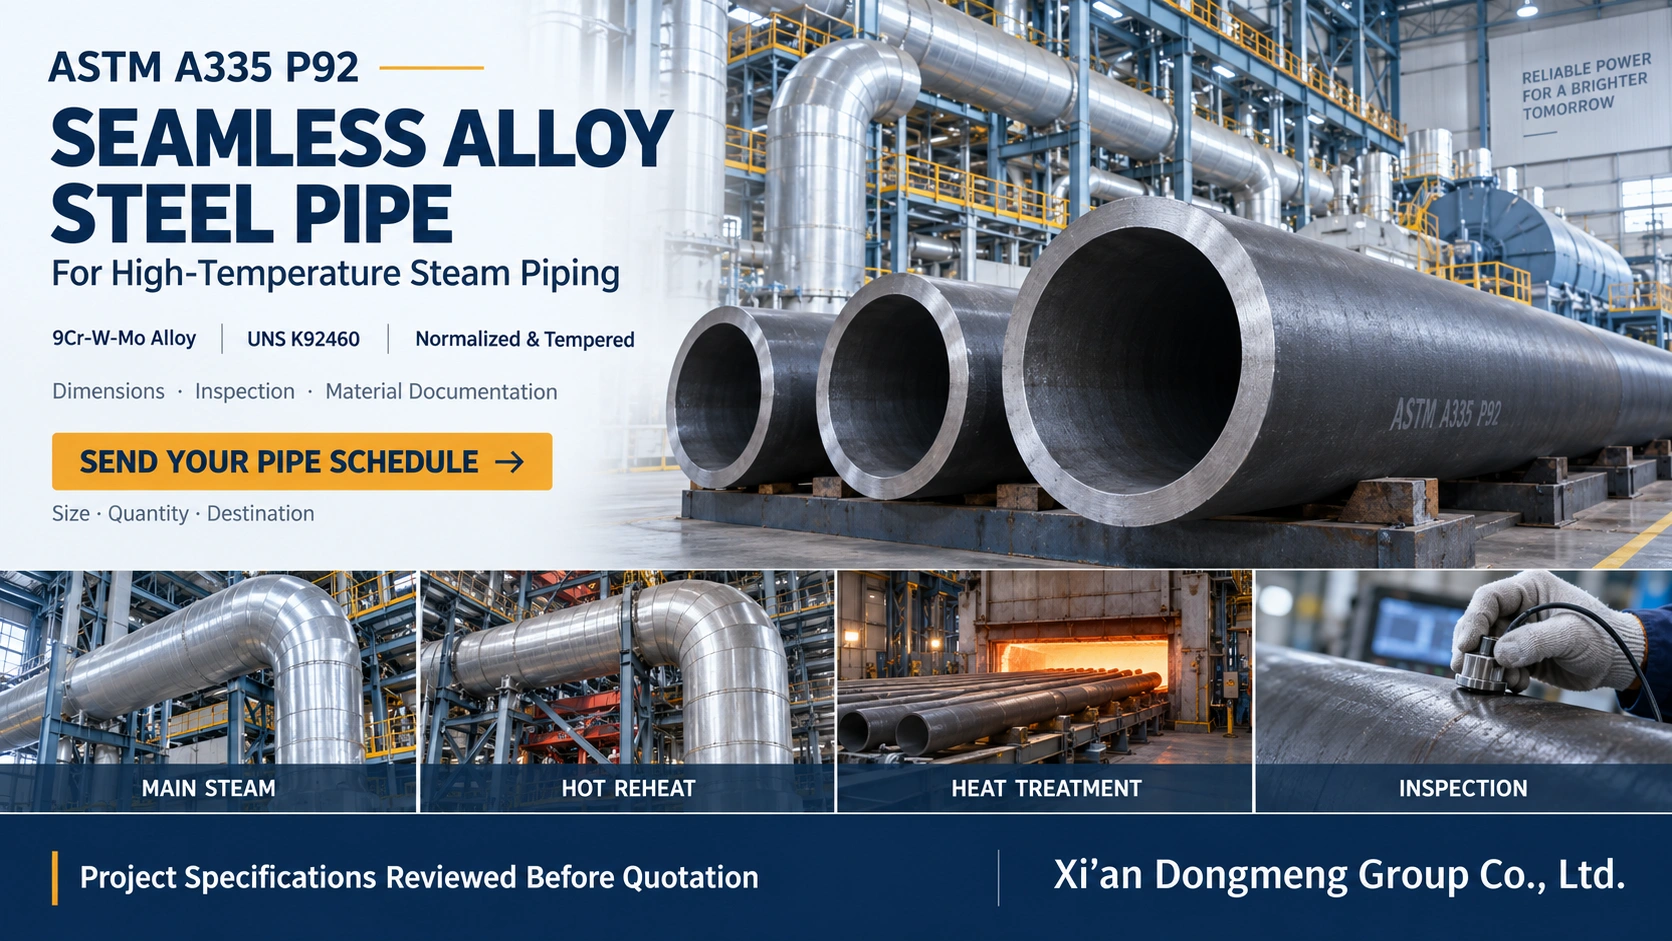
ASTM A335 P92 Seamless Alloy Steel Pipe
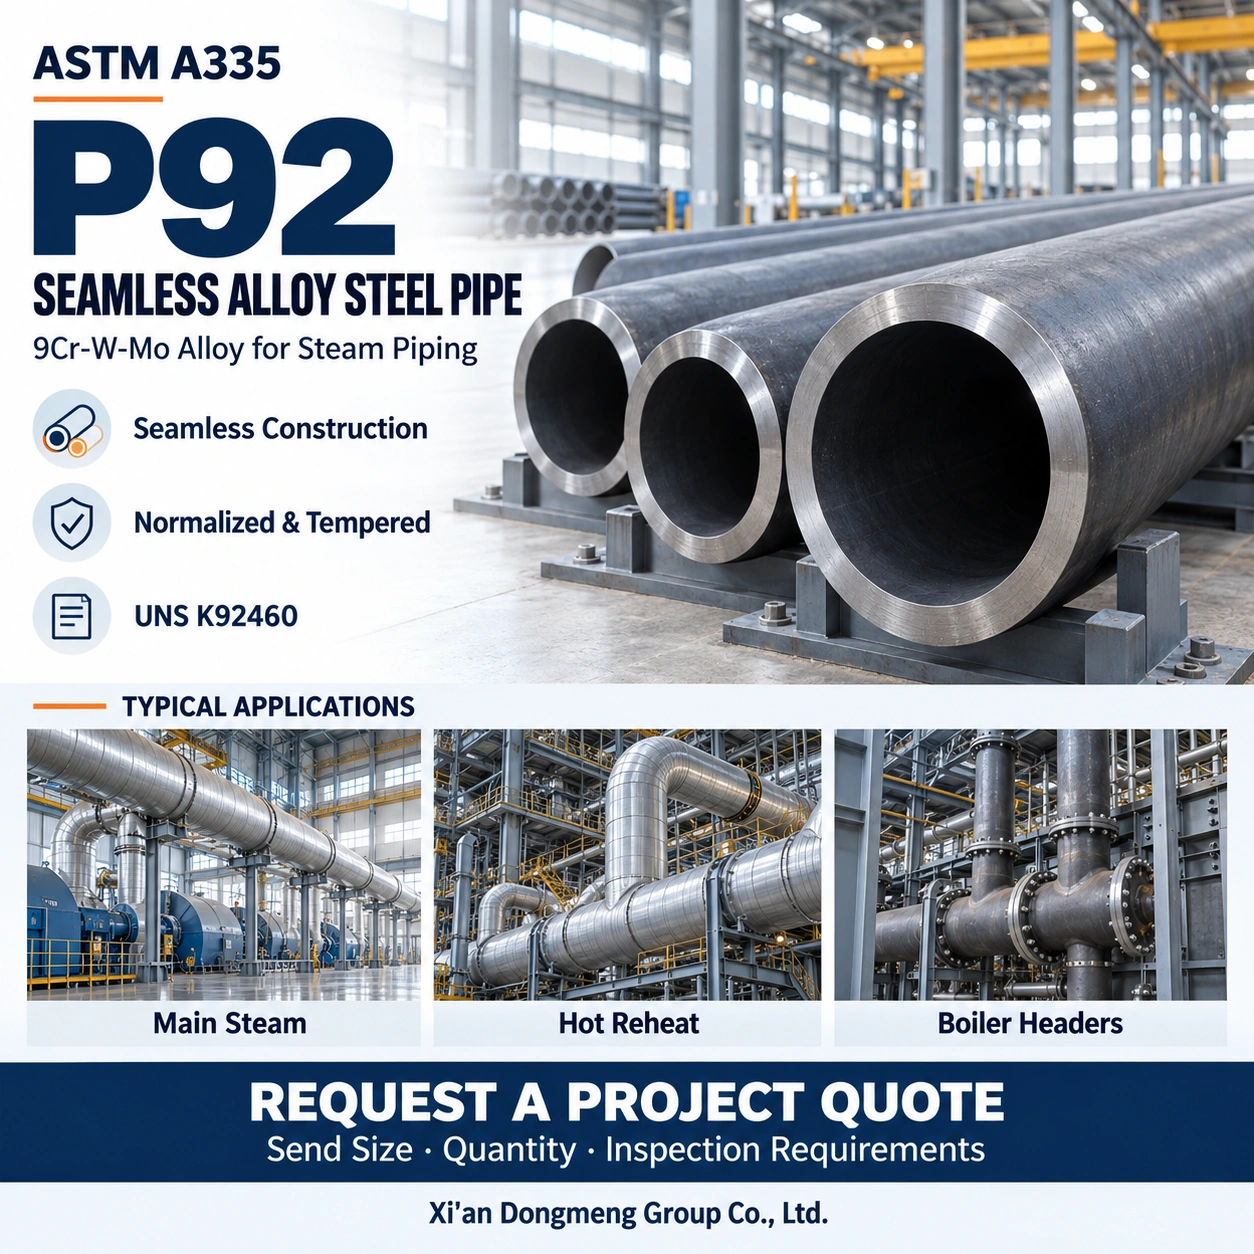
P92 seamless pipe for specified high-temperature steam piping, boiler connections and power generation projects.
Xi'an Dongmeng Group Co., Ltd. supports project sourcing of ASTM A335 P92 seamless alloy steel pipe for EPC contractors, boiler equipment manufacturers and power plant maintenance teams. Send your material requisition or pipe schedule for review of dimensional availability, heat treatment, inspection requirements and export delivery.
P92 is a tungsten-modified, approximately 9% chromium creep-strength-enhanced ferritic steel. Its alloy design supports elevated-temperature strength in demanding steam systems, provided that material condition, fabrication and operating requirements are properly controlled. Main steam and reheat piping are established applications for this grade. Technical reference: Nippon Steel boiler tube and pipe catalogue
Grade: P92
UNS: K92460
Product Form: Seamless round pipe
Delivery Condition: Normalized and tempered
Ordering Basis: NPS and schedule, or specified diameter and wall thickness
Documentation: Specify mill certification, inspection records and traceability requirements in your RFQ
Request a P92 Pipe Quote
Send your dimensions, quantities and destination, or attach your material take-off for review.
Product Specifications and Ordering Options
| Item | Specification or ordering requirement |
|---|---|
| Product standard | ASTM A335/A335M, Grade P92 |
| ASME requirement | Specify ASME SA-335/SA-335M P92 when required; certification must be confirmed for the offered material |
| General requirements | Applicable ASTM A999/A999M requirements, together with the ordered product specification |
| Manufacturing route | Seamless; hot-finished or cold-drawn route according to the ordered requirements |
| Heat treatment | Normalized and tempered |
| Diameter and wall | Specify NPS with schedule, or diameter with nominal/minimum wall thickness |
| Dimensional reference | ASME B36.10M where applicable to the ordered dimensions |
| Length | State required cut length or acceptable random-length range |
| Pipe ends | Plain or beveled ends, with preparation details agreed before ordering |
| Surface protection | Specify permitted temporary protective coating and bore cleanliness requirements |
| Inspection documents | State required certificate type and additional reports |
| Availability | Confirmed against each diameter, wall thickness, quantity and inspection scope |
ASTM A335 is a material and product specification for seamless pipe used at elevated temperatures. It does not establish a single operating pressure or temperature for every P92 pipe size. ASTM A335/A335M official scope
For heavy-wall or machined components, state whether wall thickness is nominal or minimum. Include machining allowances, end preparation, dimensional tolerances and the applicable drawing revision.
P92 Chemical Composition
The following reference limits are expressed as mass percentages and are based on the published ASTM A335/A335M-23 P92 requirements. They describe specification limits, rather than results from a particular heat.
| Element | Content, % | Element | Content, % |
|---|---|---|---|
| Carbon, C | 0.07–0.13 | Chromium, Cr | 8.50–9.50 |
| Manganese, Mn | 0.30–0.60 | Molybdenum, Mo | 0.30–0.60 |
| Silicon, Si | ≤0.50 | Tungsten, W | 1.50–2.00 |
| Phosphorus, P | ≤0.020 | Vanadium, V | 0.15–0.25 |
| Sulfur, S | ≤0.010 | Niobium, Nb | 0.04–0.09 |
| Nickel, Ni | ≤0.40 | Nitrogen, N | 0.030–0.070 |
| Aluminum, Al | ≤0.020 | Boron, B | 0.001–0.006 |
| Titanium, Ti | ≤0.010 | Zirconium, Zr | ≤0.010 |
Reference: ASTM A335/A335M-23 public preview, Table 1.
For material acceptance, review the actual heat analysis against the contract edition and any additional project restrictions. A commercial description such as "9Cr alloy pipe" is insufficient to identify P92.
Mechanical Properties
The following room-temperature reference requirements apply to the specified heat-treated material.
| Property | Reference requirement |
|---|---|
| Tensile strength | Minimum 620 MPa / 90 ksi |
| Yield strength | Minimum 440 MPa / 64 ksi |
| Longitudinal elongation | 20% for applicable standard specimen conditions* |
| Brinell hardness | Maximum 250 HBW |
Elongation requirements depend on specimen geometry, orientation and wall thickness. The 20% value must not be applied indiscriminately to thin-wall strip specimens.
Reference: ASTM A335/A335M-23 public preview, Tables 3–6.
These values support incoming material verification. High-temperature piping design additionally requires the applicable allowable stresses, creep considerations, dimensions and fabrication factors.
Heat Treatment and Fabrication Considerations
P92 is supplied in the normalized and tempered condition. Published ASTM A335/A335M-24 reference treatment ranges are:
| Treatment stage | Reference temperature |
|---|---|
| Normalizing | 1040–1080°C / 1900–1975°F |
| Tempering | 730–800°C / 1350–1470°F |
The treatment route and applicable notes must follow the ordered specification. ASTM A335/A335M-24 public preview, Table 2
For project procurement, identify any required furnace records, heat-treatment batch identification and additional verification before the order is placed.
Welding and forming
P92 fabrication requires qualified procedures appropriate to the grade, component thickness and construction code. The fabricator should establish:
Welding consumables and hydrogen control.
Preheat and interpass controls.
Welding sequence and heat input.
Post-weld heat treatment and its recording requirements.
Examination and acceptance criteria for completed joints.
Site PWHT parameters must be established through the applicable code and qualified welding procedure. The mill tempering range alone does not define an acceptable field welding procedure.
Welded P92 assemblies also require consideration of heat-affected-zone creep performance, including Type IV damage. Parent-pipe tensile results alone cannot establish the long-term performance of the completed weldment. TWI review of Type IV cracking in creep-resistant steels
P92, P91 and T92: Which Product Should You Specify?
| Material | Product focus | Procurement consideration |
|---|---|---|
| ASTM A335 P92 | Tungsten-modified Grade 92 seamless pipe | Evaluate where the approved design requires Grade 92 creep performance |
| ASTM A335 P91 | Modified 9Cr-1Mo seamless pipe | Confirm the specified grade and project requirements before considering substitution |
| ASTM A213 T92 | Grade 92 seamless boiler, superheater and heat-exchanger tubing | Purchase to the tubing specification; a P92 pipe certificate does not automatically establish T92 compliance |
| EN X10CrWMoVNb9-2 | Related European creep-resistant grade | Compare the complete product standard, testing and certification requirements before accepting an alternative |
Major producers distinguish Grade 92 pipe and tube specifications within their power-generation product ranges. Tenaris power-generation products
P92 may support wall-thickness optimization where the applicable design rules permit it. Any change from P91 requires engineering review of the full piping system, including welds, fittings, fabrication and inspection requirements.
Have an existing P91 specification? Send the material requisition and proposed change for supply review. Material substitution remains subject to the purchaser's engineering approval.
Typical Applications and Information Needed for Selection
| Application | Relevant procurement information |
|---|---|
| Main steam piping | Design temperature and pressure, construction code, dimensions and material specification |
| Hot reheat piping | Operating conditions, pipe sizes, fabrication requirements and inspection scope |
| Header and boiler connection components | Component drawings, machining allowance, wall requirements and heat-treatment provisions |
| Replacement pipe for maintenance projects | Original material records, required matching dimensions, outage schedule and acceptance requirements |
The boiler-tube and pipe applications of Grade 92 are documented by primary manufacturers. Product form must be selected correctly for each component. Nippon Steel application references
For superheater or reheater tubing, confirm whether ASTM A213 T92 is the specified product.
Inspection, Certification and Heat Traceability
An effective inspection plan identifies the examination method, acceptance criteria, sampling or coverage, and the records required for release.
| Verification area | Evidence to specify or review |
|---|---|
| Material identity and chemistry | Original mill certificate, heat number and reported chemical analysis |
| Mechanical properties | Applicable tensile, elongation and hardness results with test identification |
| Heat treatment | Delivery condition and any separately ordered treatment records |
| Dimensions and surface | Diameter, wall thickness, length, end preparation and visual inspection records |
| Hydrostatic testing and NDE | Examinations required by the contract edition and purchase order, with identifiable results |
| Project-specific testing | Additional PMI, impact testing, metallographic examination or witness points where specified |
| Shipment traceability | Connection between pipe markings, certificates, bundle identification and packing list |
Mandatory specification requirements should be distinguished from additional project inspections. Agree additional tests before production or material allocation.
PMI complements the documentation package. Alloy identification alone does not demonstrate complete chemical compliance, correct heat treatment or satisfactory mechanical properties.
If EN 10204 Type 3.1 documentation is required, state this in the RFQ and confirm the proposed certificate package before purchase. Requirements for Type 3.2 documentation or independent inspection should be raised at the same stage so the necessary arrangements can be assessed.
Send Your Inspection Specification
Attach your inspection and test plan, approved-mill requirements or documentation checklist with the inquiry.
Processing, Packing and Delivery Review
Cut lengths, end beveling, identification marking and packing requirements can be reviewed against your material requisition. Provide drawings where machining dimensions or weld preparation are critical.
For export shipments, specify:
End protection suitable for the ordered bevels and pipe dimensions.
Permitted temporary corrosion protection.
Bundle or individual-piece identification.
Supports and securing arrangements appropriate to unit weight.
Packing-list details linked to the material identification.
For material that will be cut or processed before shipment, include identification-transfer requirements so each delivered piece remains traceable.
Delivery timing depends on dimensional availability, the production route, testing, documentation review and transport arrangements. Required delivery dates should therefore be included with the initial inquiry.
Frequently Asked Questions
1. Is P92 a stainless steel?
No. P92 is a creep-resistant alloy steel used for specified elevated-temperature duties. It should not be selected on the assumption that it provides the corrosion resistance of stainless steel.
2. Are ASTM A335 P92 and ASME SA-335 P92 automatically interchangeable?
Acceptance depends on the specification and edition required by the project. Request the appropriate certification and verify it against the offered material. Dual certification must be supported by the mill documentation.
3. What is the maximum operating temperature of P92 pipe?
A single catalogue temperature cannot establish suitability. The design must consider pressure, allowable stress, wall thickness, expected service life, weld performance and the applicable construction code.
4. Does a pipe schedule define its pressure rating?
No. Schedule identifies a dimensional wall series. The allowable pressure also depends on diameter, material, temperature, tolerances and the governing design rules.
5. Can P92 replace P91 in an existing system?
Only after engineering approval. Review component compatibility, dimensions, allowable stresses, welding procedures, PWHT and inspection requirements before accepting a change.
6. Can an EN grade be offered against a P92 inquiry?
An alternative may be reviewed if the purchaser permits it. A similar alloy designation does not establish identical product requirements or automatic code acceptance.
7. Can third-party inspection be included?
Include the proposed inspection agency, witness points, hold points and reporting requirements in the inquiry. Feasibility and scheduling should be agreed before order placement.
8. What is the MOQ, and can a sample be supplied?
Minimum quantity and sample availability depend on the requested size and supply route. State whether the sample is required for dimensional evaluation, chemical verification or destructive testing.
9. What affects the price of P92 seamless pipe?
Diameter, wall thickness, length, order quantity, production availability, mill approval restrictions, processing, testing and documentation all influence the quotation. Compare offers against the same technical scope.
10. What should be checked before accepting a quotation?
Check the proposed mill, standard edition, dimensions, nominal or minimum wall basis, heat-treatment condition, inspection scope, documents, quantity, delivery terms and any stated deviations.
Request a Quotation for ASTM A335 P92 Pipe
Send your pipe schedule, material requisition or drawing to Dongmeng Group.
For an initial quotation, include:
Diameter and wall thickness, or NPS and schedule.
Length and quantity.
Required ASTM or ASME specification and edition.
Inspection and certification requirements.
Destination and required delivery date.
Any approved-mill, origin or processing restrictions.
RFQ format example - for illustration only:
ASTM A335 P92 seamless pipe; OD 219.1 mm × 20.0 mm nominal wall × 6000 mm; 20 pieces; normalized and tempered; beveled ends to drawing; EN 10204 Type 3.1 documentation; inspection to attached ITP; destination: [port].
Xi'an Dongmeng Group Co., Ltd.
Email: office@dongmjd.com
Phone: +86 157 6921 4734
WhatsApp: Contact Dongmeng Group
Office: Room 4107, Runfeng Building, Sanqiao New Street, Weiyang District, Xi'an City, Shaanxi Province, China.
Hot Tags: astm a335 p92 pipe, China astm a335 p92 pipe manufacturers, suppliers, factory


